If you’ve ever stepped into a factory that moves conveyor belts, powers packaging lines, or runs material handling equipment, there’s a good chance a R Series helical gear motor was doing the heavy lifting out of sight. As a supplier who’s worked with these motors for more than a decade, I’ve seen too many installers cut corners on mounting configurations—and end up with premature wear, noise issues, or even motor failure that could’ve been avoided with a little basic knowledge. Today, I’m breaking down what the R Series mounting configurations actually are, why they matter, and how to pick the right one for your application. R Series Helical Gear Motors

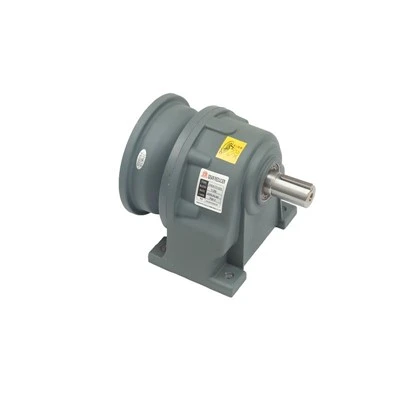
First, let’s start with the basics: R Series helical gear motors combine a helical gear transmission (those angled teeth that distribute load evenly, unlike straight-cut gears) with an electric motor, and their mounting configurations define how the entire unit attaches to a machine frame, skid, or structure. The International Electrotechnical Commission (IEC) standardized most of these configurations, which is why they’re so widely used across industrial sectors, but there are also tailored options for niche use cases.
Let’s walk through the most common mounting setups, straight from the manuals we share with every customer who buys a unit from us.
First up: Foot Mounting (IM B3). This is the most ubiquitous R Series configuration, and it’s exactly what it sounds like: two solid steel feet bolted to the base of the gear housing, with evenly spaced holes to fasten the motor to a flat machine or concrete skid. The big advantage here is stability—foot mounting distributes the motor’s weight and torque load evenly across the mounting surface, which makes it ideal for heavy, continuous applications like large conveyor systems or mixers that generate consistent vibration. I always tell customers to check that their mounting surface is flat and structurally sound; if there’s even a 1mm gap under a foot, the gear shaft will bend over time, leading to misaligned gears and increased noise. We once had a customer skip reinforcing their skid for a foot-mounted motor, and within six months, the helical gears were worn down so badly the entire unit had to be replaced—costing them three times what it would’ve taken to reinforce the skid initially.
Next, Flange Mounting (IM B5 and IM B14). Flange mounting uses a circular plate (flange) attached to the end of the gear housing, with bolt holes that align with a matching flange on the driven component (like a fan blade or a roller shaft). There are two sizes here: IM B5 is the larger, heavier-duty flange, used for motors with higher torque loads (think of large centrifugal pumps or heavy-duty screw conveyors), while IM B14 is smaller, lighter, and reserved for lower-torque applications like small packaging machines or light fans. The key thing to remember with flange mounting is shaft alignment: unlike foot mounting, which has feet to level the unit, flange-mounted motors rely entirely on the bolt holes and mating flanges to stay aligned. If even one bolt is overtightened or the flanges are slightly mismachined, you’ll get shaft runout—and helical gears need precise alignment to work properly. We include a flange alignment gauge with every IM B5 and IM B14 motor we ship, and I recommend using it every time, even if you think the alignment looks good by eye.
Then there’s Foot-Flange Mounting (IM B35). This is a hybrid of the two previous setups: it has both the feet of foot mounting and the flange of flange mounting, giving installers flexibility. You can bolt the feet to a skid for extra stability while also bolting the flange directly to a driven shaft, which is great for applications where space is tight but you need to handle a moderate torque load. A lot of our customers use IM B35 for overhead conveyor systems, where there’s not much room to attach a separate base plate, but you still need the stability that feet provide to handle the constant movement of the conveyor. One caveat here: because you have two mounting points, it’s even more important to ensure both the feet and the flange are aligned correctly—skip that, and you’ll have uneven load distribution on the helical gears, leading to faster wear.
For applications where you can’t mount a motor on a flat surface, like horizontal conveyor rails or vertical pump shafts, we offer Shaft Mounting (IM B7 and IM V5). Shaft mounting is unique because it doesn’t use feet or flanges; instead, the gear housing attaches directly to the output shaft’s end. The gear housing has a bore that fits over the output shaft, and a keyway to lock the gear and shaft together, while the motor side of the unit stays separate and is often mounted on a bracket attached to the frame. This setup is perfect for compact applications, but it’s the one I see installed incorrectly most often. The most common mistake? Not properly securing the keyway, which leads to the gear spinning on the shaft—eventually stripping the key and causing the motor to stop entirely. We always include a torque specification for the keyway when we ship a shaft-mounted R Series motor, and I advise rechecking that torque after the first 100 hours of operation, because vibration can loosen the key over time.
There’s also Vertical Mounting, which breaks down into two: IM V1 and IM V3. IM V1 is when the motor’s output shaft is pointing downward, and IM V3 is when it’s pointing upward. These are used for vertical applications like lift systems, augers that move material straight up, or submerged pumps. The big thing to watch here is lubrication: in horizontal foot or flange mounts, the gear oil circulates naturally around the helical gears, but in vertical mounts, the oil can pool at the bottom of the gear housing, leaving the upper gears under-lubricated. For this reason, we design vertical R Series motors with internal oil deflectors that keep oil flowing evenly across all gears, but you still can’t use a standard horizontal motor in a vertical application—it has to be an explicitly configured vertical R Series unit. We once had a customer try to use a standard foot-mounted R Series motor for a vertical auger, and within a month, the upper helical gears seizes because they were dry. That mistake cost them a shutdown and a new gear set—something we warn about in all our product documentation.
Now, why does choosing the right mounting configuration matter so much? It’s not just about fitting the motor into a space. The mounting setup directly affects the motor’s load capacity, lifespan, noise level, and energy efficiency. Helical gear motors rely on the precise angle of their teeth to distribute torque evenly across multiple teeth at once; if the mounting configuration causes misalignment, only a small number of teeth carry the full load, leading to accelerated wear and higher energy use. In fact, our internal tests show that a mismounted R Series helical gear motor uses up to 15% more energy than a correctly mounted one, and has a lifespan 50% shorter. For industrial operations that run 24/7, that’s a huge cost difference over the life of the motor.
I also want to note that when we supply R Series helical gear motors, we don’t just send the unit and a vague manual. We work with each customer to match the mounting configuration to their specific application, and we offer optional mounting kits for every setup. That includes shims for leveling foot-mounted motors, alignment gauges for flanges, keyway locks for shaft mounts, and oil deflectors for vertical units. A lot of suppliers will just sell you the motor and leave the rest up to you, but we’ve learned over the years that taking the time to get the mounting right upfront saves our customers a lot of hassle later.
If you’re currently dealing with an underperforming R Series helical gear motor, or you’re outfitting a new line of equipment and aren’t sure which mounting configuration to choose, we’re here to help. We’ve installed these motors in thousands of applications, from small packaging workshops to large manufacturing plants, and we can walk you through the pros and cons of each setup based on your load, space, and operating environment. Don’t risk downtime or premature motor failure by cutting corners on mounting configuration—reach out to us to discuss your needs, and we’ll make sure you get the right R Series helical gear motor with the perfect mounting setup for your operation.
Micro Gear Motor References
- International Electrotechnical Commission (IEC) Standard 60034-7: Rotating electrical machines – Part 7: Classification of types of construction, mounting arrangements and terminal box position (IM Code).
- Design of Helical Gear Drives for Industrial Applications, American Gear Manufacturers Association (AGMA) Standard 2001-B12.
- R Series Helical Gear Motor Installation and Maintenance Manual, Manufacturer’s Technical Data Sheet, 2024 Edition.
GuangDong Ruisico Transmission Technology Co., Ltd.
Guangdong Ruisico Transmission Technology Co., Ltd. is one of the most reliable r series helical gear motors manufacturers and suppliers in China, also supports customized service. Welcome to buy durable r series helical gear motors made in China here and get quotation from our factory. For price consultation, contact us.
Address: No. 70, Anjing Road, Shengfeng Community, Xiaolan Town, Zhongshan City
E-mail: info@risc-drive.com
WebSite: https://www.risc-motor.com/
